
Stainless steel machined parts
316 stainless steel resists corrosion in harsh environments and performs well in saltwater, acids, and humid conditions. That’s why you see it in marine parts, food processing equipment, and medical devices. The reason it holds up so well is its high nickel and molybdenum content. These elements improve corrosion resistance, particularly against chlorides, and enhance pitting resistance due to the addition of molybdenum.
But machining 316 stainless steel is not simple. It work-hardens quickly, and if the cutting speed is too high or the tool is not sharp, heat and pressure can cause the surface to harden ahead of the cutter. Work hardening can occur if:
- The tool is dull,
- It stops during cutting
- If the feed is too low, causing rubbing and slippage at the tool tip.
Moreover, during machining operations, heat builds up quickly if chip evacuation and coolant management are not well managed. At Ancastings, we apply these practical steps in every job. We select the best tools for the job and set the correct cutting parameters based on material hardness and part geometry. We also focus on strong workholding and proper chip evacuation, which helps us mitigate tool wear, improve surface finish, and keep production costs under control.
Keep on reading to learn about 316 stainless steel machining techniques, grades, challenges, and practical tips.
Types of Stainless Steel Grades Optimal for Machining Applications
Shiny steel automotive parts
There are various types of stainless steel. Each type behaves differently during machining: some grades cut smoothly, while others work-harden or wear tools quickly.
- 303 Stainless Steel: The easiest austenitic grade to machine is 303. It has sulfur added to its alloy to enhance chip break and reduce tool loading. As such, 303 will produce a smoother cutting operation and minimize tool wear. 303 is primarily used as a fastener material, a shaft material, or in other hardware applications where the speed is a greater concern than corrosion resistance.
- 304 Stainless Steel: Although 304 is the most common stainless steel, a strong and highly corrosion-resistant material. However, it will work harden rapidly when machined at high speeds due to its stainless steel hardness. If the cutting speed is increased too much, the material’s cutting surface will begin to harden, and the tool will wear down faster. 304 is generally used in the manufacture of food processing equipment, kitchen appliances, and general fabrication.
- 316 Stainless Steel: 316 is even more corrosion-resistant than 304, particularly in marine and chemical environments. However, the increased corrosion resistance of 316 is accompanied by greater difficulty. In comparison to machinable stainless steel 304, 316 heats up more and work-hardens more rapidly, thus requiring lower cutting speeds and/or strong coolant flow. 316 is commonly used in medical devices, marine components, and chemical equipment.
- 430 Stainless Steel: The most common ferritic grade is 430. It has better machinability than 304; it still requires proper tooling and a stable setup to achieve optimal results. 430 is typically used in appliance parts, decorative trim, and exhaust components. Due to the 430’s characteristics, you can run slightly higher cutting speeds than those required for austenitic steels; however, tool wear should still be monitored.
- 2205 Duplex Stainless Steel: 2205 is the most commonly used duplex stainless steel. 2205 is widely used in chemical, marine, and oil and gas equipment due to its exceptional corrosion resistance. However, 2205 is extremely difficult to machine due to the heavy chips it produces; therefore, you must use a strong coolant flow. Additionally, to minimize heat generation and tool wear, you must maintain a rigid setup and reduce tool rubbing.
- 17-4 PH Stainless Steel: 17-4 PH is a heat-treatable stainless steel with high strength. Similar to 416f, it is relatively easy to machine before heat treatment. However, once heat-treated, 17-4 PH becomes much more difficult to machine due to the increased hardness. It is used extensively in aerospace parts, medical implants, and high-strength industrial components. Machining 17-4 PH requires a stable setup and sharp tools to prevent work hardening.
(Also read: stainless steel 316 vs 316l)
Machining Techniques for 316 Stainless Steel
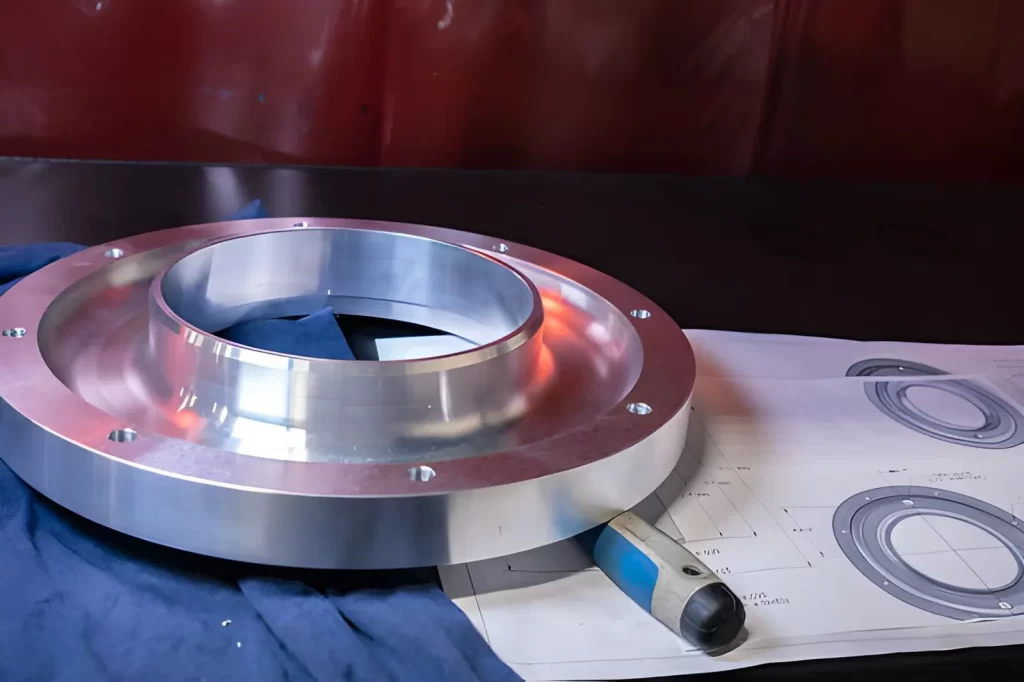
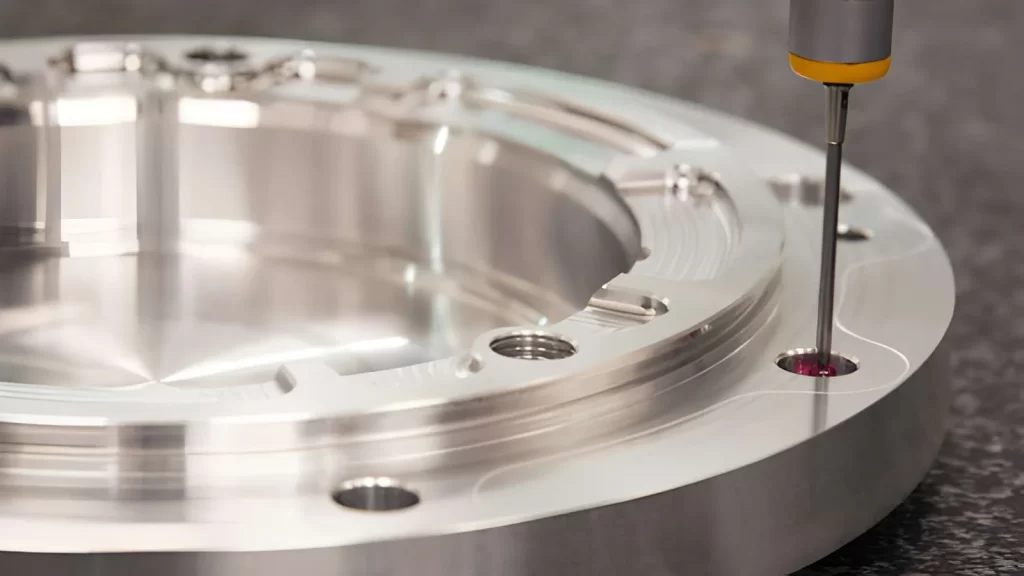
CNC-Machined Stainless Steel Flanged Ring
Machining Checklist for 316 Stainless Steel
| Parameters | Recommendations |
| Tooling | Use sharp, coated carbide with a positive rake. Avoid letting the tool sit in one spot (no dwell). |
| Parameters | Keep a steady chip load, don’t rub the tool, and use slower speeds than for mild steel. |
| Cooling | Flood with coolant or use high-pressure if you can. Aim it directly at the cutting edge. |
| Workholding | Make sure the part is held tight. Keep the tool overhang short to prevent vibration. |
| Chip Control | Use chipbreakers, peck holes, clear chips often, and follow a steady feed strategy. |
Below are the primary machining of 316 stainless steel.
- Turning 316 Stainless Steel: Turning is the most common method for shaping 316 stainless steel into shafts, pins, and cylindrical parts. The key to success is maintaining the tool as a cutter (not a rubbing tool), so the part does not work-harden (harden as it is machined). To accomplish this, use very sharp carbide inserts, feed them at a constant rate, and lower your cutting speed compared to mild steel. All of these methods will help regulate heat generation and minimise the risk of work-hardening. Additionally, having potent workholding and minimizing tool overhang will help to eliminate vibration.
- Milling 316 Stainless Steel: Milling 316 is used to produce slots, pockets, and flat surfaces. The major challenge with milling 316 is heat build-up. When the tool remains in contact with the chip, the tool becomes hot and stops cutting effectively. As a result, mill the cut lightly but steadily, and ensure that the coolant reaches the cutting area and evacuates chips effectively. Climb milling is typically an effective way to achieve a better surface finish and to reduce tool loading. Long tool extensions also cause vibration and a poor surface finish. (Also Read: milling stainless steel speeds and feeds)
- Drilling 316 Stainless Steel: Drilling 316 SS requires careful speed control and chip control. Drilling at high speeds hardens the material and dulls the tool. Use split point drills and feed them steadily. For deep holes, peck drilling helps remove chips and prevents the drill from overheating. Coolant is essential for cooling the drill, particularly for deep holes. Trapped chips in the hole can cause the drill to break or the hole to be oversized.
- Tapping 316 Stainless Steel: Most shops have failed due to inadequate planning. The material is tacky, and the chip can jam the tap. The remedy is to select the appropriate tap geometry and keep the tap cool. Spiral flute taps pull chips back, making them more suitable for blind holes, while spiral point (gun) taps push chips forward, making them ideal for through holes. Feed the tap at a moderate pace and provide adequate lubrication. If the tap begins to bind, immediately stop and remove accumulated chips. Stopping before the tap binds and removing chips will help prevent tap breakage and preserve the thread quality.
- Boring and Reaming: Boring and reaming are used when a high level of accuracy, including tight hole tolerance and smooth finishes, is required. Due to the material 316 stainless steel properties, the tool must remain stable and be fed slowly. Vibrations during boring and reaming will produce chatter marks and out-of-round holes. Coolant is essential for controlling heat. Boring is used to form bearing seats and precise bores. Reaming is used to form tight-fit holes and accurate assembly features.
- CNC Machining: CNC machining combines turning, milling, drilling, and tapping into a single operation. CNC machining is best suited for complex parts and tight tolerance requirements. The key to successful CNC machining of 316 is to develop a toolpath that minimizes tool changes and maintains consistent cutting throughout. Potent workholding and high-pressure coolant are also essential. CNC machining is ideal for producing medical parts, marine components, and chemical equipment that frequently use 316 stainless steel.
Try Ancastings Now!
Challenges With Machining 316 Stainless Steel
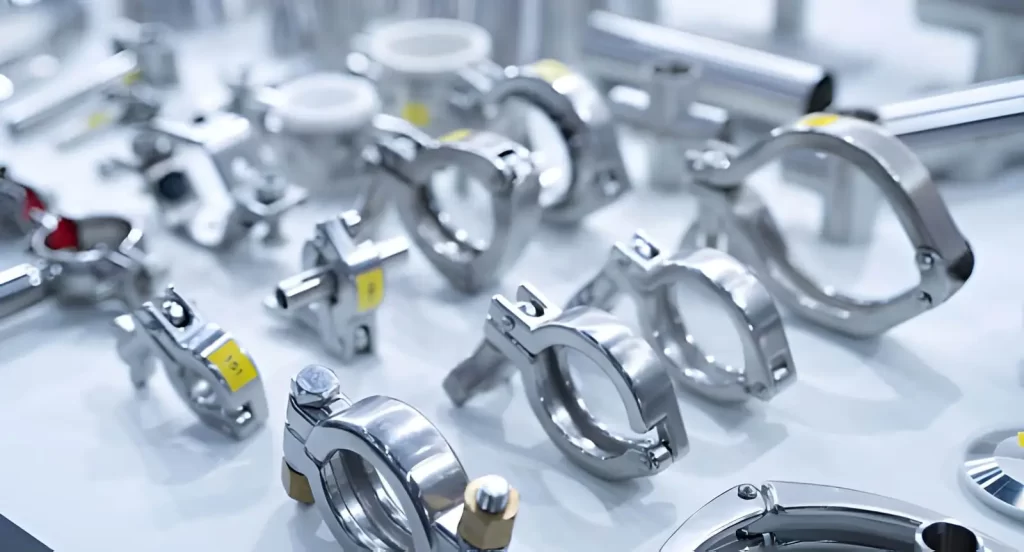
316 Stainless Steel Clamps and Pipe Fittings
There are several issues encountered when machining 316 stainless steel that can lead to poor surface finishes, rapid tool wear, and lost production time. These issues often arise from the material’s toughness and tendency to work-harden. The following are some of the most common problems you will encounter when machining stainless steel:
Work Hardening
Stainless steel tends to work-harden rapidly when the tool is allowed to rub rather than cut. This results in a hard, surface layer that is difficult to remove. If continued cutting is done without resolving this issue, both tool lives will decrease rapidly, and the part will begin to deform. Maintaining the proper speed, using sharp tools, and maintaining stable cutting conditions will minimize the occurrence of work hardening.
Tool Wear and Tool Breakage
The high heat generated by 316 stainless steel’s toughness, combined with friction during cutting, results in rapid tool wear. High-speed steel tools are especially prone to this problem. Carbide tools will last longer, but they will experience rapid tool wear if the cut is unstable. Tool breakage occurs when the tool is subjected to excessive loads or the setup is subject to vibrations. Improving tool geometry and developing a setup that minimizes vibrations will improve tool life.
Poor Surface Finishes
Surface finishes become rough when the tool vibrates, chips wrap around the tool, or the part, or the cutting speed is too high. The buildup of heat during stainless steel machining also affects the surface finish. Providing the proper coolant flow, using sharp tools, and maintaining a stable setup will improve the surface finish of the stainless steel.
Chipping Problems
Chips formed during the machining of stainless steel are long, stringy, and can wrap around the tool or part. Both the efficiency of the cutting process and the finish will be affected by these types of chip formations. Poor chip control also leads to higher tool temperatures. Improving chip breakers, increasing the feed rate, and enhancing the coolant will help manage the chips formed during stainless steel machining.
Try Ancastings Now!
Considerations and Tips to Ease 316 Stainless Steel Machining
As with any machining process, 316 stainless steel machining can be made much simpler by taking the time to plan the process and selecting the proper setup. The primary objective of machining stainless steel is to minimize heat, prevent work hardening, and keep the tool cutting. The following are useful factors to consider, along with a practical tip for producing stainless steel parts.
Use the Right Tool, Material, and Geometry
CNC-Machined Cylindrical Component
Sharp tools and strong tool material are needed for machining stainless steel. The most favourable tool material for machining stainless steel is carbide, as it can withstand heat and remain sharp longer than any other tool material. Positive rake-angle tools will also reduce cutting force. Finally, tools with good edge strength and proper chip breaker design will help prevent tool wear and improve surface finish.
Keep Cutting Speed Low and Feed Stable
High cutting speed generates heat rapidly and causes work hardening. Reducing cutting speed and maintaining a steady feed will allow for a smooth cut. Often, it is beneficial to reduce the cutting speed and slightly increase the feed rate to maintain a consistent chip load and prevent overheating.
Use Strong Coolant and Chip Control
Coolant is not optional when machining 316 stainless steel. Coolant helps to control heat and remove chips from the cutting area. Flood coolant and high-pressure coolant are preferred options for machining stainless steel. Proper chip management will prevent chips from wrapping around the tool and damaging the surface finish. Shorter chips can be achieved with improved chip breakers and higher feed rates.
Get Reliable 316 Stainless Steel Machining Services
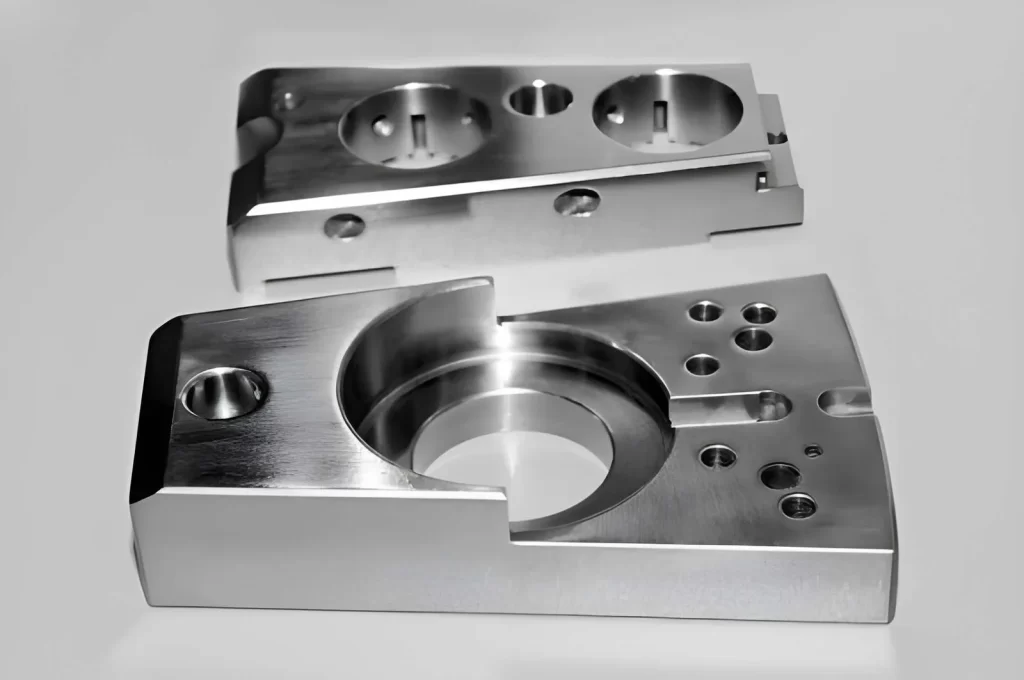
316 stainless steel industrial part with round holes
Ancastings is a leading manufacturer of custom CNC machining services. We offer a wide range of capabilities, including stainless steel cutting, CNC machining, rapid tooling, and sheet metal prototyping. Our goal is to make production simple, fast, and reliable for you.
Our approach to your project is straightforward. You share your design, and our team reviews it using objective manufacturing standards. We then plan the production and manufacture the parts in-house using modern CNC machines. This means you get advanced machining capabilities without having to invest in equipment yourself.
We also provide free DFM (Design for Manufacturing) analysis to spot potential issues early. Our pricing is transparent, with no hidden charges, and we provide clear lead times before production begins. You can also choose from a range of surface-finishing options, such as polishing, passivation, anodizing, and more, depending on your part’s needs.