
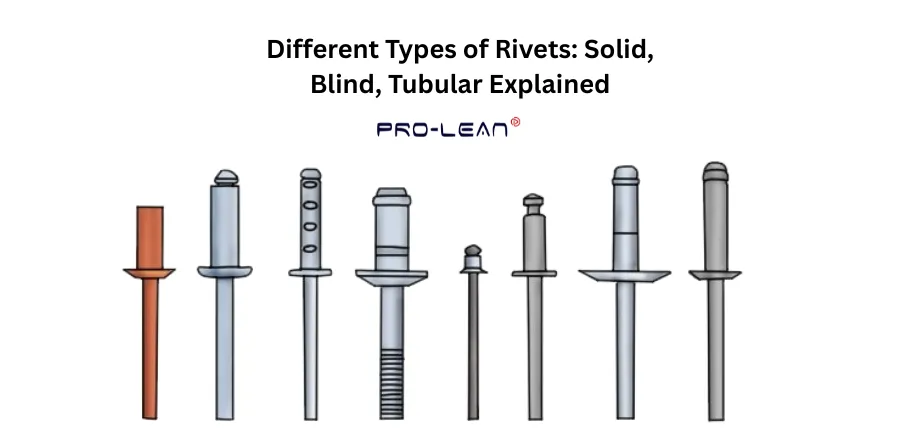
Seven Rivet Types Compared
Rivets are permanent mechanical fasteners. They have a cylindrical shaft with a head on one end. Installing rivets deforms the tail, and this secures the materials together for a strong and vibration-free joint.
There are many types of rivet fasteners, each serving a different purpose. At Ancastings, our expert assembly and DFM team can help you select the right rivet for your applications in aerospace, automotive, or sheet metal fabrication. We have a host of corrosion-resistant materials and expert rivet craftsmanship.
Working Principle of Rivets
Rivets establish permanent mechanical connections through shank deformation, which expands to match holes and creates a clamping head on the tail end. The installation process for different rivet types depends on plastic deformation to achieve load distribution.
- Solid Rivets: The rivet gun and bucking bar apply compressive force to deform the tail section, which creates a shop head with an upset height that is 1.5 times the shank diameter. The monolithic structure of this design produces high shear strength because it remains as a single piece.
- Blind Rivets: The tool extracts the mandrel from the tubular shank, which causes the body to expand both radially and axially until it reaches its designed break point to form a blind-side head without access to the rear.
- Shear Strength Calculation: The load distribution follows the formula τ = F / (πd²/4), where τ represents shear stress, F represents the applied force, and d represents the shank diameter. The maximum shear stress value before failure depends on the material’s yield strength.
Common Materials for Rivets
- Aluminum Alloys (2117-T4, 5056): The strength-to-weight performance of aluminum alloys, including 2117-T4 and 5056, makes them suitable for aircraft fasteners applications because they achieve tensile strengths of up to 40 ksi. The material’s ductility enables cold forming operations without cracking, and its natural oxide coating provides acceptable protection against atmospheric corrosion, but anodizing treatment improves its performance in humid environments.
- Carbon Steel (A307 Grade A): The high tensile strength of carbon steel rivets exceeds 60 ksi because they contain hardness elements that provide excellent fatigue resistance during cyclic loading, thus making them suitable for bridge girder connections. The zinc plating process protects carbon steel rivets from rust formation in wet environments because their uncoated surfaces develop rapid oxidation.
- Stainless Steel (304, 316): The corrosion-resistant properties of stainless steel rivets stem from their chromium content, which creates protective oxide films that protect against pitting and crevice corrosion in marine and chemical processing environments. The austenitic structure of these rivets provides ductility at cryogenic temperatures, making them suitable for pressure vessel construction.
- Copper and Brass: The high electrical conductivity of copper (58 MS/m) and thermal stability make it suitable for electrical enclosure applications that require grounding continuity. Brass contains zinc for improved machinability and antimicrobial properties, which makes it suitable for plumbing fixtures that need to prevent biofouling.
- Monel (Nickel-Copper Alloy): The corrosion-resistant properties of Monel rivets make them suitable for offshore oil platforms because they withstand acidic and saline environments while maintaining tensile strengths of up to 70 ksi.
- Titanium Alloys (Ti 6Al-4V): These deliver high strength-to-weight ratios (tensile up to 130 ksi) and superior biocompatibility, essential for medical implants and aerospace components exposed to extreme temperatures, as they resist creep and maintain integrity beyond 400°C.
Quick Selection Table for Rivets
| Rivet Type | Common Rivets | Main Uses | Main advantage |
| High Load Structural | Solid, huck (lockbolt), Blind rivets | Structures like bridges and aerospace | High shear and tensile strength |
| Single Sided Rivets | Blind rivet, Closed end, multi-grip | One sided assemblies, industrial machines | Medium strength |
| Thin Rivets, Low Load, Rivets | Tubular, Split | Leather, plastics, and wood | Low strength |
What Are the Different Kinds of Rivet Heads
Round Head
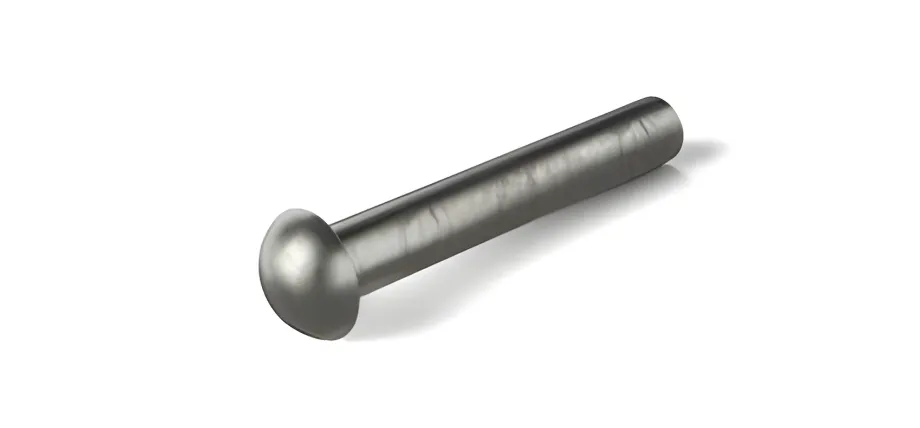
Round Head Solid Rivet
The round head contains a convex dome design, which creates an enlarged contact area (1.5-2 times the shank diameter) to distribute pressure evenly. The manufacturing process of the head includes machining or forming to prevent sheet pull-through while maintaining a height that equals 0.4 times the diameter.
Flat Head
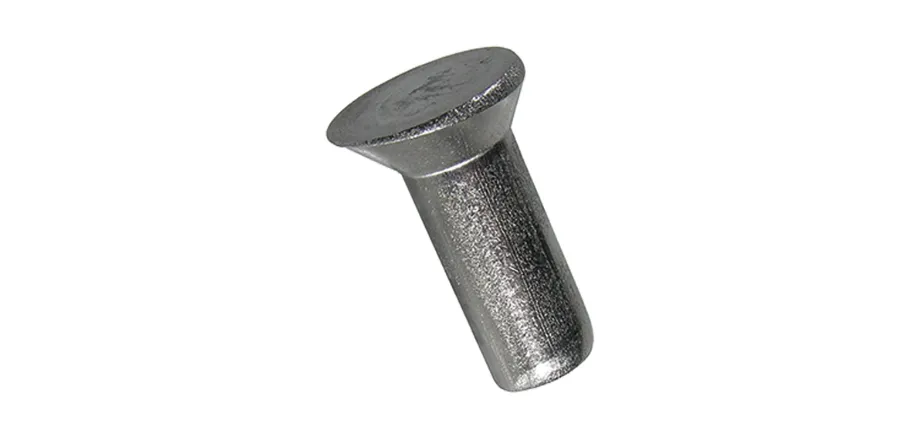
Countersunk Head Flat Head Rivet
Flat heads offer a planar surface flush with the material, minimizing protrusion for applications requiring smooth exteriors. The head diameter is standardized at twice the shank diameter, ensuring stable clamping without countersinking.
Countersunk Head
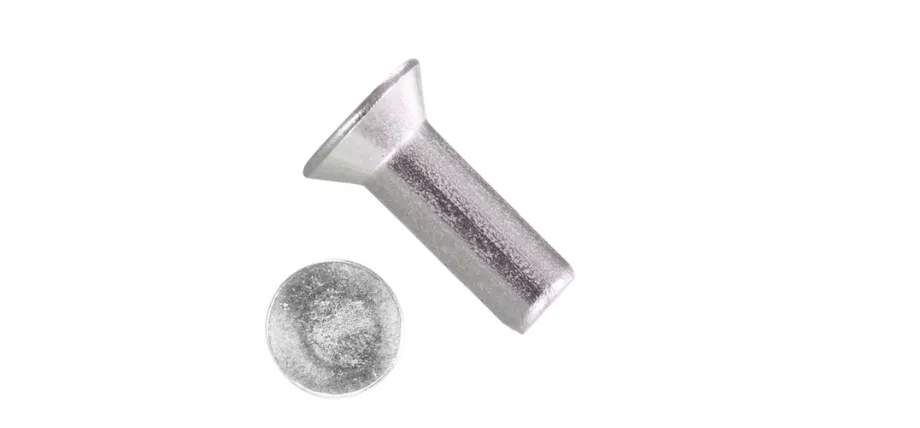
Countersunk Head Solid Rivet
The 100° or 120° tapered design of countersunk rivet heads allows them to sit flush inside chamfered holes. This creates a smooth surface, which is especially useful in sheet metal assembly for aerospace, automotive, and other applications where reduced drag and a clean finish are important. The 100° head angle also provides good load distribution around the joint.
Pan Head
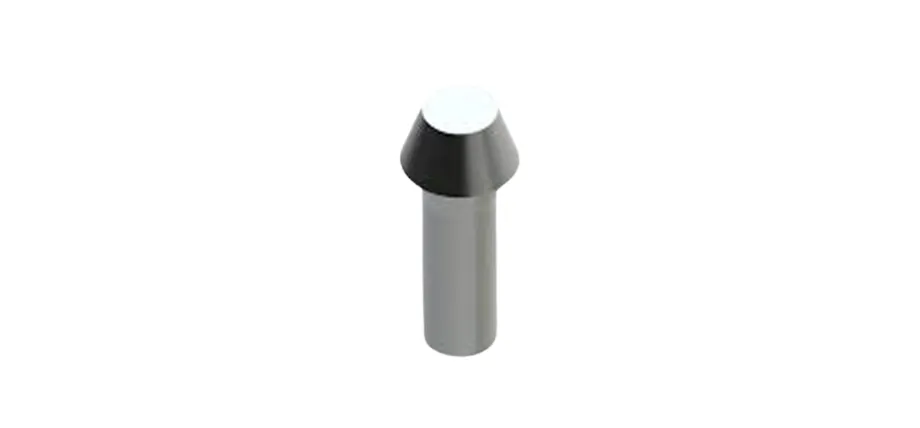
Pan Head Solid Rivet
The Pan head design features a rounded top section that meets a flat base, providing both structural support and clear visibility. The head height measures 0.6 times the diameter size, which works for environments with moderate vibration that do not require full flush embedment.
Truss Head
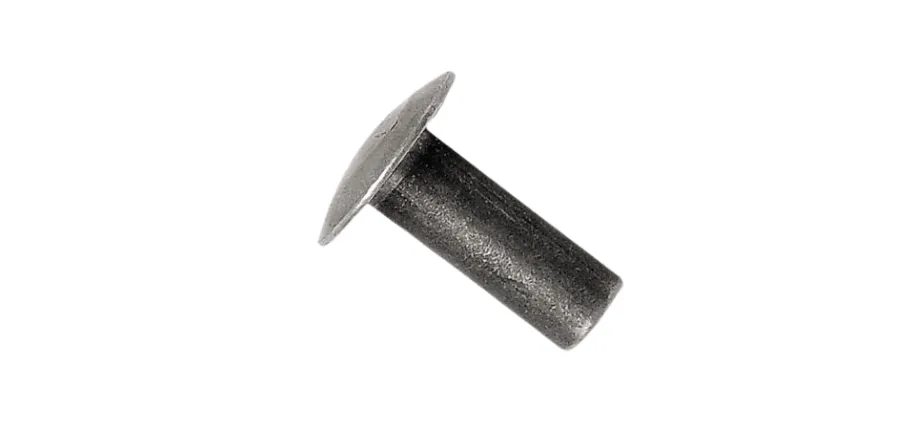
Truss Head Solid Rivet
The truss head design features a flat, wide dome with an inward curve that spreads the weight distribution across three times the diameter of the shank, preventing composite materials from cracking.
Large Flange Head
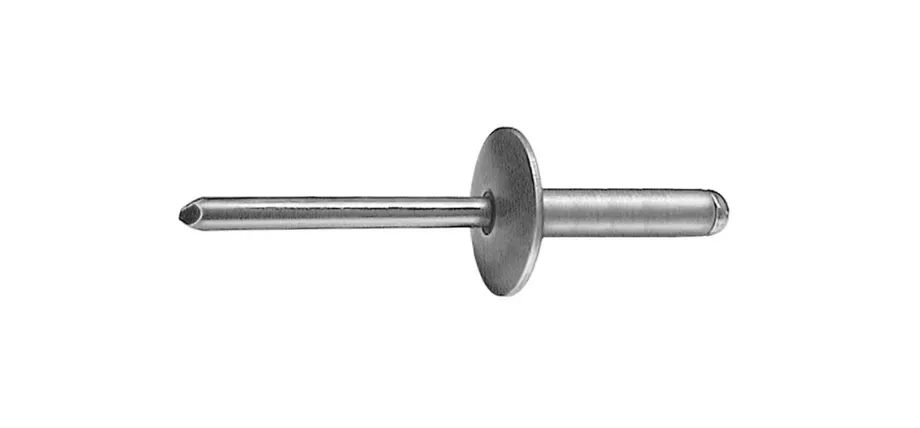
Large Flange Blind Rivet
The extended washer-like base of large flange heads provides better pull-out resistance when working with soft materials. The flange diameter of these fasteners reaches more than four times the size of their shank, which makes them suitable for plastic joint applications that require high tension.
Different Types of Rivets
Solid Rivet
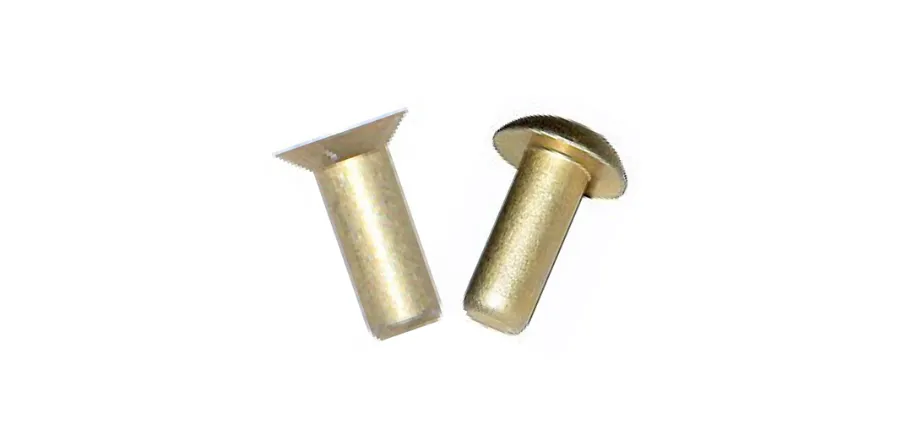
Brass Solid Rivets Comparison
The installation of solid rivets requires bucking the tail to form a secondary head through cold or hot deformation of the material. The single-piece construction, featuring solid rivets, yields high shear strength values that reach 80-90% of the parent material’s ultimate tensile strength, while also providing excellent fatigue performance under cyclic loading. The manufacturing process includes heading and trimming operations to achieve exact dimensions while allowing shank lengths to reach ten times the diameter for deep insertion applications.
- The structural components of aerospace fuselages and wing skins require vibration resistance that exceeds 10^6 cycles.
- Shipbuilding uses hull plates to withstand corrosive saltwater exposure during operation.
- Heavy machinery frames operate under static loads that exceed 50 tons.
Blind (Pop) Rivet
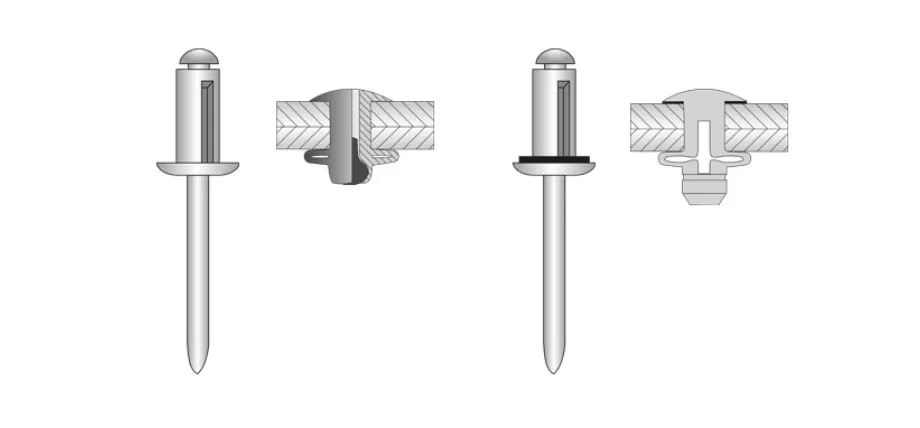
Standard Open-End Blind Rivet
The design of blind rivets, also known as pop rivets, includes a mandrel that extends from a tubular body when pulled, creating a shank expansion that results in a hidden head section. The installation process of these rivets takes less than five seconds when using pneumatic tools, achieving shear strengths between 200 and 500 lbs for 1/8-inch diameters. The shank diameter determines the grip range, which spans from 0.5 to 2 times the diameter of the shank.
- Automotive fasteners in body panels serve as essential components that support the operation of fast-paced assembly production lines.
- HVAC ductwork seals all joints to prevent air from escaping.
- Thin PCBs through enclosure design, which prevents access to the backside of the printed circuit boards.
Tubular Rivet
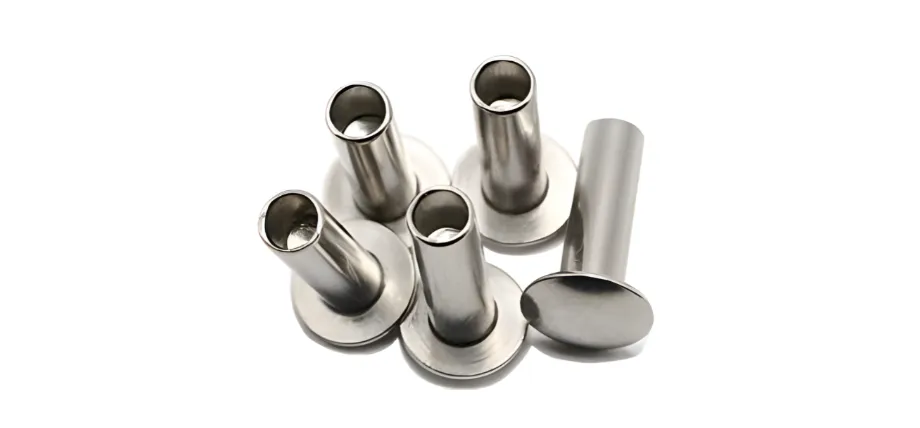
Tubular Rivets Assortment
Tubular rivets are another type of rivet with a hollow shank. The installation process of tubular rivets creates a clinch joint through their partially hollow shank, which becomes rolled or flared at the tail end. The hollow design of these rivets achieves a 30-40% weight reduction compared to solid rivets, while requiring 50% less deformation force for installation, making them suitable for automated pressing operations.
- The materials of leather goods and upholstery remain intact because they pierce through soft materials without causing any tears.
- The design includes rivets in sheet metal that protect appliances through their pivot mechanisms.
- The application of plastic assemblies in consumer packaging requires only minimal shear forces.
Semi-Tubular Rivet
Semi-tubular rivets have a shallow dimple (0.2-0.3 times the shank length) at the tail, which enables deformation with 20-30% less force than solid rivets while maintaining 70-80% of the shear capacity. The dimple starts to control upset, which helps prevent irregular material flow.
- The brake linings and clutch plates in vehicles experience wear due to the continuous friction they encounter.
- Ladders and scaffolding, which maintain their position to support human body weight while people move around.
- Furniture frames and furnishings provide cost-efficient, permanent connections.
Full Tubular Rivet
Full tubular rivets feature a deep, hollow shank that extends 70-80% of their length, enabling complete clinching with minimal axial force. However, their shear strength drops to 50-60% of that of solid rivets due to the void. The design suits situations where wires or fluid need to pass through.
- The lighting fixtures and signage sections contain conduit integration points through their joint connections.
- Soft, pliable bindings—whether draped over books or fashioned into bag straps—act as a protective veil, sparing the substrate from harm.
- Medical device housings serve to enable the drainage of sterile fluids.
Try Ancastings Now!
Split Rivet
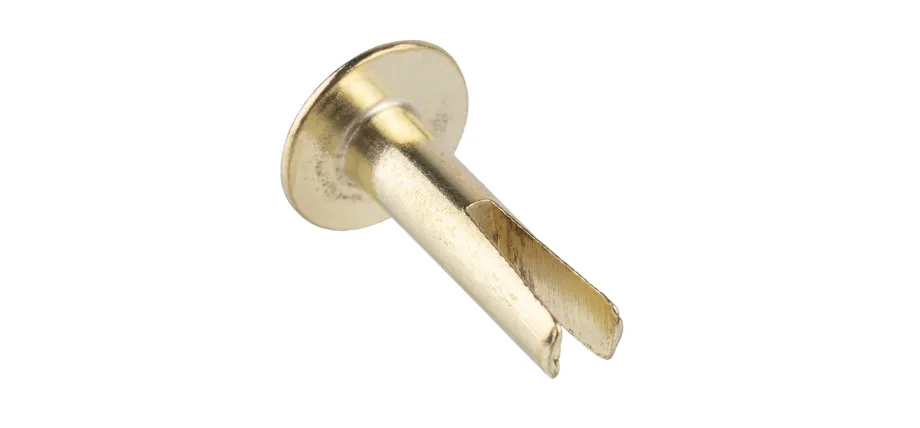
Split Rivet
The split rivet design features a divided shank that widens upon insertion to secure fibrous materials without requiring pre-drilled holes. The prongs of these rivets expand at a 45-60° angle to generate wood pull-out forces of up to 300 pounds, while their self-piercing feature facilitates easier field installation.
- The process of upholstery and canvas tent construction involves using frames to hold fabrics in place.
- The system features wooden crates and pallets that can be disassembled as needed.
- The distribution of tensile forces occurs through leather belts and harnesses, which maintain uniform stress distribution.
Compression Rivet
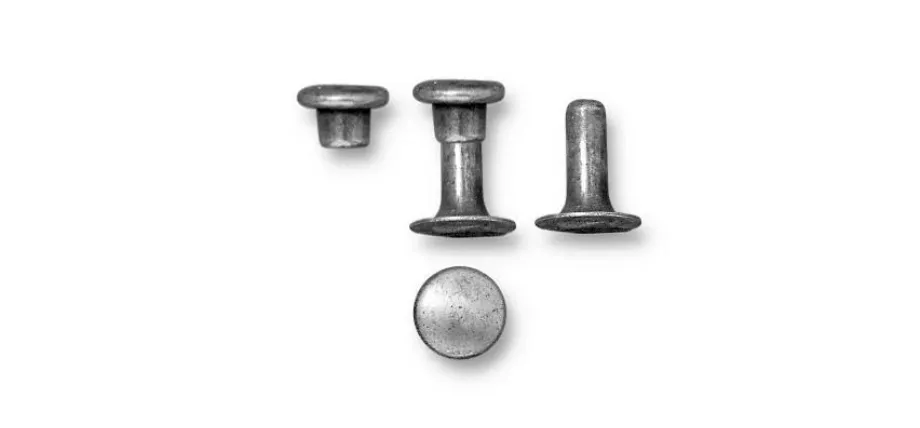
Compression Rivet Components
The two-part design of compression rivets features a tubular body and a solid stem that merge through an interference fit to expand the shank diameter by 0.01-0.02 inches. The design produces uniform clamping pressure through standard tools, making it suitable for mass manufacturing operations.
- They are commonly used in leather goods such as handbags.
- Textile reinforcements in sails function to oppose wind shear forces.
- The packaging includes straps that create tamper-evident seals.
Drive Rivet
Drive Rivets Pair
The drive rivet design features a short mandrel that extends from the shank to create radial expansion when hammered, eliminating the need for tool extraction. The installation process requires 40-50% less force than pop rivets while the mandrel stays inside to provide additional shear strength of up to 400 pounds.
- The construction process requires formwork to serve as temporary plywood sheathing, fastened in place.
- The marine deck fittings need to withstand wave impacts.
Flush (Countersunk) Rivet
The tapered head of flush rivets fits completely into countersunk holes, creating a smooth surface because they do not extend beyond the material. The 100° angle remains intact through deformation, while the bearing surface maximizes its strength for tensile forces acting across the joint plane.
- The aircraft skins function to decrease drag when operating in transonic flight conditions.
- Automotive trim panels enhance aesthetic uniformity.
- The design of bicycle frames achieves weight reduction through the use of minimal materials while maintaining aerodynamic performance.
Friction-Lock Rivet
Multi-Grip Blind Rivet
The locking collar of friction-lock rivets creates frictional shear resistance that exceeds 100 ksi through axial compression of grooved pins. The interference fit, ranging from 0.005 to 0.010 inches, creates a vibration-proof retention system that operates without the need for adhesives.
- Used in light aircraft repair operations where only single-sided access is available.
- The missile casings function to protect against explosive forces that occur during launch.
- Offshore rig platforms are susceptible to corrosion due to exposure to saline environments.
Huck Rivet (Lockbolt)
Huck Structural Rivet
The Huck rivet system uses a threaded or grooved pin with a collar that receives 20-30 ft-lbs of torque to create a swaged lock, which distributes forces evenly. The system achieves a 150 ksi tensile strength through its design, which includes a retained stem for improved multi-directional stability.
- The truck chassis assemblies experience excessive torsional stress.
- Wind turbine towers are designed to withstand powerful gale-force winds.
- The lockbolt requires railcar couplings that operate under high-fatigue rail conditions.
Explosive Rivet
The pyrotechnic charge inside explosive rivets ignites through heat or induction, creating a rapid shank expansion that reaches speeds of 1000-2000 ft/s to establish a sealed connection. The process of full deformation occurs within milliseconds, making it suitable for use in dangerous or distant locations.
- The process of oil field pipeline repair involves making sealed connections under high pressure without the need to disassemble any components.
- The system includes nuclear reactor baffles, which maintain containment integrity.
- The satellite solar arrays operate in vacuum space when they deploy their systems.
Peel Rivet
Peel Blind Rivet
The mandrel break creates multiple concentric rings of Peel rivets, which remove shank layers to fill voids in ductile materials, thus increasing pull-through resistance by 50% compared to standard blind rivets. The grip range of these rivets reaches three times the diameter of the material.
- Wind turbine blades utilize composite panels that are attached to honeycomb cores through bonding operations.
- Plastic automotive interiors help prevent cracks from spreading.
- Brittle ceramic fixtures function to distribute the concentrated forces that occur at specific points.
Grooved Rivet
Grooved Blind Rivet
The shank of grooved rivets features circumferential serrations that penetrate substrates during expansion, creating a stronger frictional bond that reaches 2-3 times the original strength in porous materials. The grooves reach a depth of 0.005 inches to prevent the rivet from rotating when torque is applied.
- The structural beams made of wood serve to improve the resistance against withdrawal.
- The fiberglass boat hulls function to prevent water from entering the vessel.
- Foam insulation panels serve as building materials in low-density construction assemblies.
Multi-Grip Rivet
Multi-Grip Blind Rivet
Multi-grip rivets feature a staged mandrel breaking process, which creates progressive bulges to achieve an equal clamping force. The shear values maintain stability throughout different thickness ranges, which decreases inventory requirements by 70%.
- HVAC coil fins operate with different fin spacing configurations.
- The appliance casings are constructed from mixed-gauge sheet metal.
- The frames of solar panels need to accommodate thermal expansion requirements.
Closed-End Rivet
Closed-End Blind Rivet
Closed-end rivets feature sealed tail ends, which function as seals after installation to prevent fluid or gas entry, while achieving IP67-level protection against environmental factors. The mandrel inside the enclosure enhances tensile strength by 20%, allowing it to withstand pressure differences of up to 100 psi.
- Waterproof electronics serve as essential components for marine navigation systems.
- The fuel tank baffles contain volatile vapors.
- Medical tubing connectors serve to preserve and confirm sterility.
Structural Blind Rivet
Structural Blind Rivet Setting
The mandrel of structural blind rivets remains in place through interlocking systems, which enable one-sided access to achieve a bolt-like tensile strength of up to 200 ksi. The rivet can fill holes that are 120% larger than its standard diameter, accommodating manufacturing variations.
- The bridge deck reinforcement system shows its strength when vehicles strike it.
- The system operates as a crane boom section to protect equipment from strong winds.
- Seismic building braces serve as earthquake-resilience systems.
Try Ancastings Now!
How to Select the Right Type of Rivet
- Evaluate Load Requirements: Finite element analysis determines the shear, tensile, and fatigue requirements for the design, which selects solid or lockbolt types of fasteners when loads exceed 1000 lbs while maintaining a minimum factor of safety of 1.5.
- Assess Material Compatibility: The selection of rivet alloy must match the substrate materials through galvanic series testing to prevent corrosion. Stainless steel is best suited for harsh chemical environments, while aluminum is suitable for non-ferrous materials.
- Determine Grip Range and Hole Fit: The assessment of grip range and hole fit requires measuring the total thickness plus 1.5 times the diameter for protrusion length. Production needs multi-grip variants when thickness variations exceed 20%.
- Consider Installation Access and Tools: The selection of blind rivets becomes necessary for single-sided operations, but users must verify that their tools match production requirements within 10 seconds per joint.
- Account for Environmental Factors: The selection process requires sealed or corrosion-resistant options for environments with moisture and temperature fluctuations exceeding 200°C and chemical exposure. Perform tests according to ASTM F606 standards.
- Review Cost and Assembly Efficiency: The selection between initial expenses and operational efficiency requires evaluation, as tubular rivets minimize deformation energy by 40% for low-load, high-volume applications.
Custom Sheet Metal Fabrication
Ancastings offers high-quality sheet metal fabrication services with material guide, inspection, and assembly services. We provide a host of post-machining and fabrication surface finishes and joining methods, including:
- Riveting
- Welding (laser and spot welding)
- Soldering
- Brazing
- Bolting & Hemming
Request a free quote today and get optional DFM support when starting production.
Conclusion
Rivets are important for sheet metal fabrication and are the standard method for joining panels and metal sheets without heat or affecting the material. Selecting the right type of rivet is important for structural integrity and reliable joints. The distinction between the different types of rivets allows you to pick vibration-dampening, shear strength, and material, which ensures the joints have a long life and survive wear and impacts.
FAQ
What are rivets used for?
Rivets are used to permanently join materials together. They are commonly used in sheet metal fabrication, aerospace applications, and automotive panels, where they provide strong, vibration-free connections.
What is the difference between riveting vs welding?
The main difference between riveting vs welding is the type of joining. Rivets join the material mechanically without heat or direct material distortion. Welding uses heat to thermally fuse the material.